
Aerospace CNC Machining in China: Materials, Documentation, and Tolerance Expectations That Survive Verification
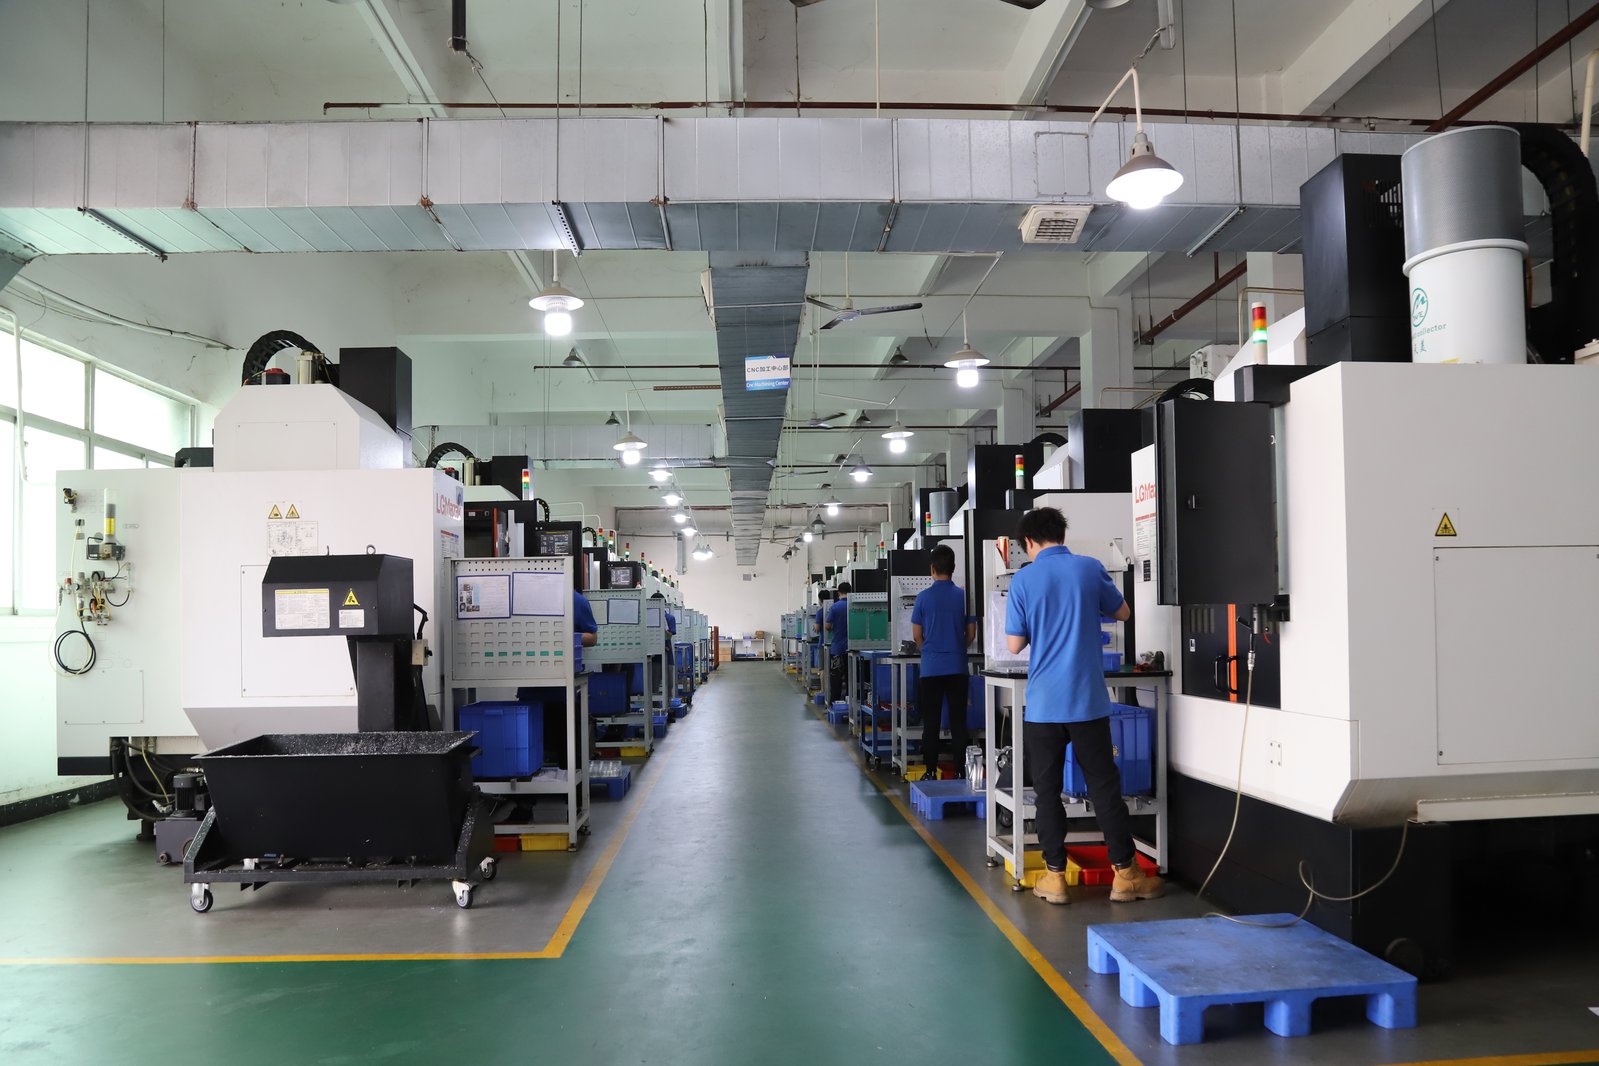
Aerospace parts sourced from China are bought on documentation as much as on dimensions, because the industry's risk sits in the material and the process record as much as in the machined feature. This guide is the buyer's reality check for aerospace CNC machining work. It covers the materials and material states that carry most of it, the tolerance and finish expectations that are realistic from a certified machining floor, and the documentation chain that must survive an audit. It is written from the verification-first view this site applies to every claim: name the evidence before you commit.
Why does aerospace machining in China come down to verification?
Aerospace is the industry where the gap between a claim and a record is widest, and where that gap costs the most. A machined bracket for a commercial aircraft program may be a simple geometric part, but it flies in an environment where fatigue, material traceability, and process control are regulated expectations, not preferences. When the machining happens in China, the buyer cannot walk the floor daily, so the verification chain has to travel with the parts instead. Material certificates name the alloy and standard. XRF records state what actually reached the machine. CMM reports carry the dimensions, and lot-level traceability ties every part back to its material and its process.
There is an honesty boundary every buyer should hear first. A machining floor holds ISO 9001, IATF 16949, and ISO 14001, not AS9100, and not NADCAP. That is not a shortcoming for build-to-print aerospace hardware; it is a scope statement. The IATF 16949 certificate covers the manufacture of CNC machined metal parts and explicitly excludes product design under Clause 8.3, which means this floor takes a released aerospace drawing and machines it to print. Suppliers who claim aerospace design authority or NADCAP-certified processes without the certificates to back them are the first thing an audit should eliminate.
Which materials and material states carry most aerospace machining work?
Aerospace CNC work concentrates in a handful of material families, each with its own verification demands. The materials a certified machining floor sees most often:
- 7075-T6 aluminum — the aerospace structural default. High strength-to-weight, widely specified for airframe brackets, fittings, and structural hardware. Its verification is the temper: 7075-T6 is not interchangeable with 6061 or 5052, and a certificate naming the alloy without the temper is only half the document. T7351 (over-aged for stress-corrosion resistance) appears where the drawing demands it.
- Ti-6Al-4V (Grade 5) and its ELI variant (Grade 23) — the strength-and-fatigue metals. Titanium is bought for strength-to-weight, toughness, and fatigue behavior — properties that chemistry predicts but does not prove. Grade 5 and Grade 23 share the same aluminum and vanadium chemistry; the difference is the oxygen limit, and that difference is invisible to an XRF spectrometer. Aerospace titanium therefore demands a mill certificate read against the standard (ASTM B348 for bar, or the Chinese GB/T 2965 designation) and, where the drawing requires it, confirmation of the ELI chemistry from the certificate rather than from a floor instrument.
- 17-4 PH stainless — the high-strength corrosion-resistant option. Machined in the annealed (Condition A) state and then precipitation-hardened to H900 or H1150 for strength. The verification is the treatment record plus hardness after aging, because the chemistry alone does not prove the final properties.
- High-temperature alloys when the drawing names them. Inconel-class nickel alloys appear in turbine-adjacent hardware. They machine slowly, demand rigid setups, and are usually specified for parts that see heat — a conversation about process capability and cycle time, not just chemistry.
The pattern a buyer should internalize: in every aerospace material family, the document that matters is the one that proves the state — the temper, the heat treatment, the ELI chemistry, the mill lot — not just the family name. A certificate that names the alloy and the standard, read against the drawing, is where aerospace material verification starts. The material-verification sections of this site's guide walk through the same checks for each metal family in full.
Which tolerance and finish expectations are realistic on a machined aerospace part?
Aerospace drawings carry real tolerances, but "aerospace precision" is not a single number — it is a feature-by-feature expectation routed to the process that can hold it. On this floor the working standard is the same one the rest of the site quotes: milling and turning hold ±0.003 mm, and precision grinding holds ±0.002 mm on bearing seats, sealing faces, and roundness-critical diameters. What aerospace adds is the reason those numbers matter — fatigue — and the discipline that follows from it.
Surface finish in a fatigue environment is not cosmetic. A rough surface or a sharp internal edge is a stress raiser, a place where a crack can start under cyclic load, which is why aerospace drawings call finish on functional faces and why edge break is a real callout rather than an afterthought. Realistic finish expectations run the same ladder as any precision work — Ra 3.2 µm standard machined, Ra 1.6 µm fine machined, Ra 0.8 µm with a finishing pass or light grinding, Ra 0.4 µm and finer by grinding or polishing — with the coarse end reserved for non-critical faces and the fine end for the surfaces that carry load or seal.
The buyer-side rule for aerospace tolerance and finish: call the tight numbers only where the part uses them, name the finish on the faces that matter, and expect the verification documents to cover exactly those callouts. A drawing that blankets the part in ±0.003 mm and Ra 0.8 everywhere is not more "aerospace" — it is more expensive, and it forces inspection time onto faces that will never see a fatigue cycle.
How does a machined part's geometry set the tolerance it can honestly hold?
The geometry rules that govern any machined part apply with extra force in aerospace, because the materials are harder to cut and the consequences of a failed feature are higher. The features that set the honest tolerance on an aerospace part:
- Thin walls and thin floors. Aerospace structural parts are often weight-optimized down to thin sections. Below a practical minimum, the wall deflects under cutting force and chatters out of tolerance no matter what the machine is rated for. The DFM conversation — thicken the wall, add a rib, relax the tolerance on a non-load path — belongs before the quote, not after the first article fails.
- Deep, small-diameter holes. Long tools deflect and chips struggle out. A deep hole that is routine in aluminum becomes slow, careful work in titanium, and the depth-to-diameter ratio decides whether the feature holds its position or wanders.
- Sharp internal corners and edge conditions. A cutter leaves a radius, so an internal corner cannot be machined square. In a fatigue part, a sharp internal corner is also a stress raiser even where it can be cut, which is why aerospace drawings specify radii and edge breaks deliberately rather than leaving them to the shop.
- Long, thin, small-diameter features. Shafts and pins that need a guide bushing close to the cut run on Swiss-type turning; without that support the bar deflects and the diameter drifts.
- Threads and fasteners features. Threads in hard materials need the right tooling and chip management, and thread callouts should be standard sizes a shop can actually cut and gauge.
The discipline is the same as in the rest of machining, intensified: tolerance belongs on the feature that needs it, and the drawing should be written so the geometry never asks the material to do something it cannot. A DFM review that flags these features during quoting is not a delay — it is the difference between a part that holds its numbers and a part that discovers them on the CMM.
What documentation should an aerospace machining lot actually carry?
Aerospace documentation is where the industry's verification expectations become concrete. A lot of machined aerospace parts should arrive with a chain that ties the material to the machine to the measurement:
- The material certificate, read against the standard the drawing names. For aluminum, the certificate carries the alloy and temper; for titanium, the alloy and the standard (ASTM or GB/T); for 17-4 PH, the condition before aging. The certificate is the document the whole material verification hangs on.
- The XRF record for incoming material. The certificate states what the mill shipped; the XRF reading states what actually reached the machine. Between the mill and the machine there are warehouses and handling where a mixed or substituted lot is cheapest to catch, which is why incoming stock here is XRF-checked before it is cut.
- The CMM report for the dimensions. The report should list nominal values, measured values, and deviations per checked feature, not a "pass" stamp. Critical dimensions are verified on Hexagon CMMs, and the report ships with the parts.
- Process capability where the drawing demands it. A single measured part proves that part; Cpk proves the process. Key characteristics are held to Ppk ≥ 1.67 initial with SPC documented per lot, so the buyer can see whether the tolerance is being held as a process or hit on a lucky part.
- First-article inspection per revision. The first-article report is available before production is released, and for regulated work it feeds a PPAP package. Every revision of the drawing should generate a fresh first article, because a change to the print can change what must be measured.
- Lot-level traceability. The MES/ERP chain records the batch, the machine, the operator, and the inspection results behind each part. When something goes wrong, traceability is what turns "one bad part" into "these lots, these machines, this material" — the difference between a rework and a recall.
None of these documents is unique to aerospace — they are the same verification chain this site applies to every order — but aerospace is the industry where every link of the chain is expected to survive an audit. The quality system page details the measurement instruments and process-capability standards behind each report, so the documents in the crate can be read against the floor that produced them. A supplier that runs the chain on every lot, under the three certificates it holds, is one whose aerospace documentation you can actually rely on.
How do you turn aerospace material, documentation, and tolerance expectations into an RFQ?
An aerospace RFQ to a Chinese CNC supplier should carry more than the drawing. It should state, in terms the supplier can quote against:
- The material by grade and standard. "7075-T6 per AMS 4045" or "Ti-6Al-4V per ASTM B348" is a spec. "Aluminum" or "titanium" is a hope, and a Chinese supplier will machine exactly what the drawing names.
- The tolerance and finish expectations per feature. Call ±0.003 mm on the features that need it, ±0.002 mm and grinding on the roundness-critical surfaces, and state the Ra on the functional faces. The RFQ should make clear which features carry the tight numbers and which live on the general block.
- The documentation package. State that the order ships with the material certificate, XRF record, CMM report, SPC data where required, and first-article inspection per revision. Suppliers who cannot commit to the documents in the quote will not produce them in the crate.
- The verification boundary. Name the certificates the supplier actually holds — ISO 9001, IATF 16949, ISO 14001 — and confirm the work is build-to-print under the IATF scope. If the program requires AS9100 or NADCAP, say so before the drawing is sent; a supplier that claims them without the certificates is disqualified by that claim alone.
- The revision and change control. State that every drawing revision triggers a fresh first article and updated records, so the documentation never drifts from the part being shipped.
Specified this way, the RFQ sorts suppliers before the geometry is sent. A certified floor that runs the verification chain answers with the documents and the process; a trading desk answers with reassurances. In aerospace, the reassurances are the risk.
How do you check an aerospace machining lot at the receiving dock?
The receiving check is where the documentation chain meets the parts. The order that arrives should reconcile in five steps:
- Read the drawing revision against the first-article report. The parts must match the current revision, and the first article must have been generated for that revision, not for an earlier version of the print.
- Check the material certificate against the drawing and the XRF record. The alloy, temper, and standard on the certificate should match the drawing, and the XRF reading should match the certificate. A mismatch at this step is a stop-ship, not a note for later.
- Verify the CMM report covers the tight callouts. The report should show measured values for the features the drawing tolerances at ±0.003 mm or ±0.002 mm, not a generic sampling of easy dimensions.
- Confirm the finish and edge conditions. Ra on the functional faces and edge break where the drawing calls it are inspection points, not assumptions. A fatigue part with a burr or a sharp edge at a stress point has a defect the drawing never authorized.
- Reconcile the lot count and traceability. The number of parts, the lot records, and the machine data should tie out. If the count does not match the records, the traceability chain has a hole, and in aerospace, a hole in the chain is the same as no chain.
The receiving check is the last line of the audit, and it is the one the buyer actually controls. Every document the RFQ demanded and the supplier committed to becomes a checkable item at the dock, so the documentation package is specified before the order, not requested after the parts arrive.
Frequently Asked Questions
Can Chinese CNC machining suppliers make aerospace parts?
Yes, for build-to-print aerospace hardware. A certified floor machines released aerospace drawings — brackets, housings, fittings, and structural parts — in aerospace materials such as 7075-T6, Ti-6Al-4V, and 17-4 PH, to ±0.003 mm with grinding at ±0.002 mm, with the full documentation chain. The boundary is honest: this floor holds ISO 9001, IATF 16949, and ISO 14001, not AS9100 or NADCAP, and the IATF scope excludes design. Suppliers who claim aerospace design authority or NADCAP without certificates should be eliminated in the audit.
What materials are used for aerospace CNC machined parts?
The most common are 7075-T6 aluminum for structural hardware, Ti-6Al-4V (Grade 5) and its ELI variant (Grade 23) for strength-to-weight and fatigue duty, and 17-4 PH stainless for high-strength corrosion-resistant parts. High-temperature alloys such as Inconel appear where the drawing calls for them. Each family has its own verification demand — the temper for aluminum, the ELI chemistry for titanium, the treatment record for 17-4 PH.
What tolerance can an aerospace CNC machined part hold?
Milling and turning hold ±0.003 mm, and precision grinding holds ±0.002 mm on bearing seats, sealing faces, and roundness-critical diameters. The realistic expectation is feature-by-feature: tight numbers on the features that carry load or seal, general tolerances on the rest. Aerospace does not change what a machine can hold — it changes how carefully the tolerance and its verification are specified.
Why is titanium verification different from aluminum in aerospace work?
Because the property that matters most is invisible to the common floor instruments. Grade 5 and Grade 23 titanium share the same aluminum and vanadium chemistry; the difference is the oxygen limit, which an XRF spectrometer cannot read. An aerospace titanium claim therefore rests on the mill certificate read against the standard, and where the drawing requires ELI, the certificate is the evidence, not a floor reading.
Does a supplier need AS9100 to machine aerospace parts?
That depends on the program. Many build-to-print aerospace programs accept suppliers certified to ISO 9001 and IATF 16949 with the full documentation chain, especially for non-flight-critical hardware. Some prime contracts require AS9100 or NADCAP. The rule for a buyer: state the requirement before the RFQ, and verify the certificate against the registrar — a supplier that claims a certificate it does not hold is disqualified by the claim.
What documents should arrive with an aerospace machining order from China?
The material certificate naming alloy and standard, the XRF record for incoming material, the CMM report with measured values per feature, SPC data where process capability is required, the first-article inspection per revision, and lot-level traceability through the MES/ERP chain. Request the list in the RFQ, not after the parts ship — a supplier that commits to the documents up front is one whose process you can audit.
How do I verify the material in an aerospace part I receive from China?
Read the three layers together: the mill certificate naming the alloy, temper or grade, and standard; the XRF record stating what actually reached the machine; and, where the material's critical property is not visible to XRF — the ELI oxygen limit in titanium, the aging state of 17-4 PH — the certificate or treatment record that proves it. A mismatch at any layer is a stop-ship.
Planning an aerospace machining order from China, and not sure which material, tolerance, or documents the drawing should demand?
Send the drawing and the program's requirements. We will come back with the material and verification expectations the part realistically needs, and the documentation package the order will carry. Email [email protected] or call +86 13126536955.